# Static Electricity Hazards in Pharmaceutical Solvent Handling
In pharmaceutical and fine chemical manufacturing, static electricity is one of the most insidious hazards. Unlike fire hazards from open flames or hot surfaces, static charges accumulate silently as liquids flow, powders pour, or filters spin. If this accumulated charge reaches a threshold potential and discharges as a spark in the presence of flammable solvent vapors or dust clouds, a catastrophic fire or explosion is inevitable.
To protect personnel and equipment, process safety engineers must evaluate static hazards across the entire product lifecycle—from raw material storage to final packaging.
# 1. Charge Generation Mechanisms & Reactor Sizing
Electrostatic charge is generated whenever two dissimilar materials come into contact and then separate (triboelectric charging). In liquid handling, this occurs at pipe walls, pump impellers, and nozzle interfaces.
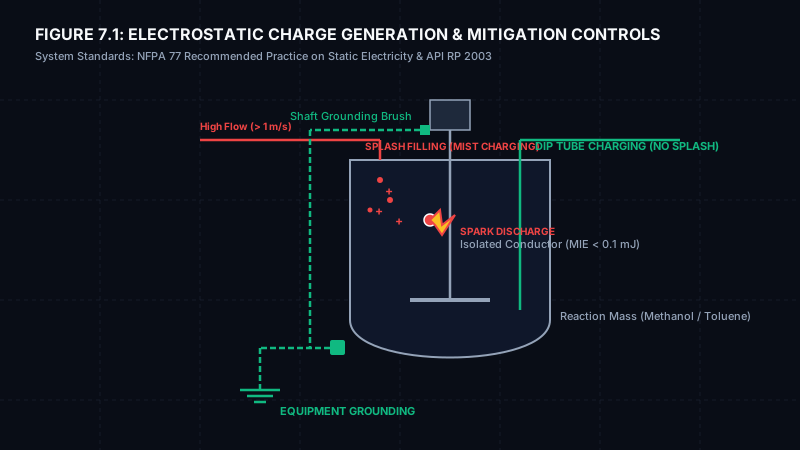
# 2. Electrostatic Hazards Throughout the Product Lifecycle
# Phase 1: Raw Material Storage & Bulk Transfer
- Bulk Unloading: Pumping solvents (such as toluene, heptane, or ethyl acetate) from road tankers to tank farms generates high streaming currents. Low-conductivity solvents are particularly hazardous because they trap charge for long periods.
- Flow Velocity Limits: NFPA 77 limits solvent flow velocity to 1.0 m/s during initial charging, until the discharge pipe is completely submerged. Once submerged, velocity must stay below 3.0 m/s (for low-conductivity fluids) or 7.0 m/s (for high-conductivity fluids).
# Phase 2: Powder Dosing & Reactor Charging
- Pouring Solids: Charging dry powders (excipients or raw intermediates) through a reactor manway creates triboelectric charge as particles slide against each other. This generates a dense dust cloud inside the reactor headspace.
- Containment & Inerting: Manual charging must occur under a continuous nitrogen sweep (reducing oxygen concentration below 2% by volume). Alternatively, closed powder transfer systems using Type C FIBC bags (which must be grounded) must be used.
# Phase 3: Mixing & Agitation
- Agitator Isolation: Agitator shafts are supported by bearings lubricated with oil, which acts as an electrical insulator. The rotating shaft can become an isolated conductor, accumulating charge from the reaction mass.
- Mitigation: Carbon grounding brushes must be installed on the rotating shaft to provide a low-resistance path (less than 10 Ohms) to ground.
# Phase 4: Filtration & Slurry Separation (Centrifuges / Nutsches)
- Filtration Friction: Forcing a solvent slurry through a filter cloth or metal mesh in a Nutsche filter generates high static potentials. If the metal filter plate is ungrounded, it can discharge a high-energy spark.
- Mitigation: Ensure MOC continuity. Ground the filter mesh and use conductive synthetic filter bags.
# Phase 5: Drying (Fluid Bed Dryers & Vacuum Dryers)
- Granular Friction: In Fluid Bed Dryers (FBD), dry granules are suspended in high-velocity air streams. This continuous contact and friction generate massive static fields.
- Mitigation: Use conductive filter bags with integrated stainless steel threads, and interlock the dryer shell to ground.
# Phase 6: Final Packaging & Warehousing
- Polyethylene Liners: Pouring dry finished API into plastic drums lined with polyethylene bags creates a high static charge on the bag surface. If the operator reaches in with a metal scoop, a spark can jump.
- Mitigation: Use dissipative plastic liner bags and grounded stainless steel scoops.
# 3. Expert Safety Parameters: Resolving Key Process Safety Gaps
As static electricity experts, process safety engineers must account for several critical electrostatic properties to ensure safe plant operations:
# 3.1. Solvent Charge Relaxation Time
When a low-conductivity solvent (like heptane, hexane, or toluene) is transferred through a pipe, it accumulates charge. Even after entering a grounded vessel, the charge remains trapped inside the bulk liquid because the liquid itself is resistive. The time required for this charge to dissipate is called the relaxation time:
- Relaxation Rule: A relaxation hold period of at least 30 to 100 seconds must be enforced after pump shutdown before inserting any manual dipsticks, sampling cups, or probes into the liquid. This allows the charge to safely drain to the grounded reactor walls.
# 3.2. Minimum Ignition Energy (MIE) vs. Human Capacitance
To put static energy into perspective, compare the energy needed to ignite solvent mists to the energy a human body can generate:
- MIE of Solvent Vapors: Typical flammable solvents (e.g., methanol, toluene, THF) have an MIE of 0.1 to 0.2 millijoules (mJ). An invisible, tiny spark is enough to trigger ignition.
- Human Capacitance Energy: A human body walking across an ungrounded floor can easily accumulate an electrostatic potential of 10,000 Volts, translating to an accumulated energy of 10 to 30 millijoules (mJ). This is 100 times higher than the MIE of solvent vapors.
- Mitigation: Operators must wear static-dissipative safety shoes (resistance between 10^5 and 10^8 Ohms) and stand on conductive or dissipative flooring. Synthetic clothing (nylon/polyester) must be banned in favor of anti-static cotton uniforms.
# 3.3. Flange Bridging Jumper Straps
Pipe flanges are joined together using bolts and internal gaskets. Gaskets are often made of non-conductive materials like Teflon (PTFE). This isolates the piping segments, converting them into isolated conductors that accumulate charge from fluid shear:
- Requirement: All piping flanges in solvent service must be bridged using conductive copper bonding straps (jumper wires) to maintain electrical continuity across the entire pipeline.
# 3.4. Continuous Grounding Loop Interlocks
Grounding clamps are subject to wear, corrosion, and operator error (forgetting to attach the clamp to the drum or tanker):
- Interlock Integration: Central transfer pumps must be interlocked with a continuous grounding monitoring system. The pump must be programmed to trip or fail to start if the grounding clamp loop resistance exceeds 10 Ohms.
# 4. Real-World Industrial Incidents & Root-Cause Case Studies
Electrostatic ignitions rarely leave physical evidence of an external ignition source, which historically led investigators to incorrectly blame "mechanical spark" or "electrical short circuits." The following industrial incidents demonstrate the exact physics of static discharge in pharmaceutical API and fine chemical operations:
# Incident Case 1: Toluene Splash-Filling Vapor Cloud Flash in 5,000 L Glass-Lined Reactor
+─────────────────────────────────────────────────────────────────────────────+
|               INCIDENT ANATOMY: TOLUENE TOP SPLASH DISCHARGE                |
+─────────────────────────────────────────────────────────────────────────────+
|  [Top Nozzle Pump-In: 5.8 m/s] ──> Liquid Jet Free Falls 2.2 m              |
|                                       │                                     |
|               Droplet Breakup & Fine Aerosol Generation                     |
|                                       │                                     |
|  [Streaming Current: 4.8 µA] ──> Charge Trapped on Liquid Surface (75 kV)   |
|                                       │                                     |
|  [Spark Jump to Ungrounded SS Dip-Pipe] ──> Exceeds Toluene MIE (0.24 mJ)  |
|                                       │                                     |
|             💥 DEFLAGRATION -> Manway Blown Off, ₹4.2 Crore Damage           |
+─────────────────────────────────────────────────────────────────────────────+
# Incident Sequence & Mechanism
During batch solvent make-up at an API intermediate plant, pure Toluene (conductivity , extremely non-conductive) was pumped from a road tanker into a Glass-Lined Steel Reactor (GLR).
- The Deviation: A bottom dip-pipe had been detached during cleaning and was not reinstalled. The operator routed the solvent through a top 3-inch nozzle, resulting in a free-fall splash drop of .
- Flow Velocity: The transfer pump delivered solvent at , far exceeding the safe initial rate of .
- Electrostatic Physics: Splash dropping sheared the liquid into a dense droplet aerosol cloud. The streaming current into the vessel reached . Because glass lining is electrically insulating (), accumulated charges could not drain to the steel shell ground. An electric potential exceeding developed across the liquid surface.
- Ignition: As the liquid level rose, a brush discharge jumped from the charged toluene surface to an isolated ungrounded stainless steel thermowell sheath. The discharge energy () easily exceeded the Minimum Ignition Energy (MIE) of toluene vapor (), triggering an immediate vapor deflagration.
# Damage & Impact
- Vessel manway lid sheared off; roof blast panels blew open.
- Two operators suffered second-degree burns.
- Production downtime: 45 days. Total asset damage and business interruption: ₹4.2 Crore.
# Incident Case 2: Manual Intermediate Powder Charging Through Open Manway
# Incident Sequence & Mechanism
At a secondary synthesis plant, an operator was instructed to charge of micronized API intermediate powder into a reactor containing of Methanol heated to (flash point of pure methanol: ).
- The Deviation: The powder was packed inside standard 25 kg low-density polyethylene (LDPE) plastic bags. The operator stood on a wooden pallet and tipped the plastic bags directly into the open manway.
- Electrostatic Physics: The powder particles sliding over the high-dielectric LDPE bag generated massive triboelectric separation charges. The bag surface charged to . Simultaneously, the operator was wearing insulating street rubber gumboots (resistance ) rather than static-dissipative safety shoes, turning the human body into an isolated capacitor accumulating ().
- Ignition: When the operator's hand brought the charged plastic liner within of the grounded stainless steel manway collar, an electrostatic spark jumped from the operator's hand to the rim. The spark passed directly through the methanol vapor plume emerging from the open manway. A flash fire erupted instantly.
# Damage & Impact
- Flash fire engulfed the mezzanine platform, destroying instrumentation cables and pneumatic tubing.
- Zero fatalities due to rapid overhead deluge activation, but the cleanroom suffered severe soot contamination.
- Facility decontamination and requalification cost: ₹1.6 Crore.
# Incident Case 3: Centrifuge Cake Scraping Spark in Heptane-Wet Slurry
# Incident Sequence & Mechanism
During isolation of an intermediate in a vertical top-discharge basket centrifuge, heptane was used for final cake washing.
- The Deviation: After spinning at 1,000 RPM, the operator opened the centrifuge lid to scrape residual wet cake from the basket wall using a manual spatula.
- Electrostatic Physics: The drive V-belts on the centrifuge were standard non-conductive synthetic rubber. Over months of operation, belt slip had coated the drive pulley with an insulating glaze, isolating the basket shaft (). As the slurry was centrifuged, the shear force generated high charge density on the rotating basket.
- Ignition: The operator used an ungrounded stainless steel scraper with a wooden handle. Bringing the conductive metal blade near the charged cake induced a spark that ignited heptane vapors ().
# Damage & Impact
- Basket internal explosion ruptured the sight glass; fire spread to the mother liquor receiver.
- Total asset loss, basket rebuilding, and downtime: ₹85 Lakhs.
# 5. Comprehensive CAPA Framework: Corrective & Preventive Action Matrix
To eliminate static ignition risks permanently, API manufacturers must execute systematic CAPA protocols addressing hardware, instrumentation, chemistry, and operational behavior:
| Safety Domain | Identified Root Cause | Corrective Action (Immediate Fix) | Preventive Action (Long-Term Engineering Control) | Verification & Monitoring KPI |
|---|---|---|---|---|
| Liquid Transfer | Splash filling & excessive flow velocity generating streaming currents. | • Install bottom-extending dip tubes with cut tip within of bottom. • Throttle pump discharge valve. | • Automate two-stage pump control: limit velocity to until liquid level submerges dip tube by , then ramp to . • Install vortex breakers to prevent two-phase gas entrainment. | Flow transmitter interlock verified on DCS every 6 months. |
| Piping & Equipment Continuity | Isolated conductors caused by insulating PTFE/PFA gaskets between flanges. | • Retrofit all pipeline flanges with cross-bonded braided copper grounding jumpers. | • Specify PTFE gaskets with integrated conductive spiral-wound stainless steel cores (e.g., GORE-TEX with conductive inserts or 316L inner rings). • Eliminate unbonded flexible PTFE braided hoses; replace with internally grounded conductive hoses. | Flange-to-flange loop resistance verified during quarterly preventive maintenance. |
| Glass-Lined Equipment | Insulating glass shell prevents static drainage from bulk non-conductive solvents. | • Install tantalum grounding tips or Hastelloy bottom outlet valves with conductive grounding lugs. | • Equip glass-lined agitator blades and baffles with fused conductive tantalum alloy strips that provide an uninterrupted discharge path to earth. • Install grounding carbon brushes on agitator rotating drive shafts. | Agitator-to-ground resistance continuously monitored; alarm if . |
| Powder Charging | Triboelectric charging from manual plastic bag dumping over open manways. | • Ban non-conductive LDPE bags in solvent rooms. • Require nitrogen purge before opening manway. | • Install closed Pneumatic Vacuum Powder Transfer Systems (PTS) operating under recirculating nitrogen. • For drum emptying, enforce Type C FIBC conductive bags with interlocked grounding clamps or conductive antistatic liner bags (). | Limiting Oxygen Concentration (LOC) interlocked to before charge valve opens. |
| Centrifuges & ANFDs | Isolated rotor basket and static charge accumulation during slurry spinning. | • Clean pulley shafts and ground basket bearing housings. | • Replace open centrifuges with hermetically sealed Agitated Nutsche Filter Dryers (ANFD). • If centrifuges are retained, install antistatic conductive drive belts (ISO 1813), conductive filter bags with sewn stainless steel wire grids, and automated nitrogen inerting. | analyzer in vent line trips inerting gas if . |
| Personnel & PPE | Human body capacitance () discharging through ungrounded boots. | • Issue static-dissipative safety footwear () and cotton lint-free uniforms. | • Install daily Electrostatic Discharge (ESD) Turnstile Testers at solvent block entries: operators must test footwear & wristbands; access door unlocks only upon passing test. • Apply conductive epoxy flooring throughout solvent handling areas (). | 100% daily turnstile pass log audit recorded in EHS compliance dashboard. |
# 6. Engineering Preventive Measures & Quantitative Design Formulas
# 6.1. Safe Solvent Flow Velocity Criteria (NFPA 77 / API RP 2003)
The streaming current () generated by fluid flowing through a conductive pipe of diameter at linear velocity is governed by:
To keep the streaming current well below the electrostatic charge generation threshold:
- Initial Flow Rule (Unsubmerged Nozzle):
- Submerged Flow Rule (Low-Conductivity Solvents, ):
(where is internal pipe diameter in meters and is velocity in m/s).
3. High-Conductivity Solvents (, e.g., Alcohols, Ketones):
# 6.2. Minimum Relaxation Time Hold Rule
For low-conductivity hydrocarbons (Toluene, Heptane, Hexane, Cyclohexane), the electrostatic relaxation time constant () is:
Where , is the relative dielectric constant ( for toluene), and is electrical conductivity ().
To ensure complete charge dissipation to less than of peak potential, process safety standards require a holding period of at least before lowering any conductive dipstick, sampling bottle, or thermocouple into the liquid.
# 6.3. Continuous Grounding Loop Interlock Architecture
Standard spring clamps with rusty jaws fail silently. Modern pharmaceutical plants must install Intrinsically Safe (Ex i) Grounding Monitoring Systems (e.g., Newson Gale Earth-Rite / ATEX Zone 0/20 certified):
- The system injects a micro-current signal through the clamp jaws.
- It verifies both ground loop resistance () and capacitance signature (ensuring the clamp is clipped to a real metal vessel or drum, not to a painted rail or isolated bolt).
- The dry contact interlock is wired in series with the tanker pump starter circuit: if the ground resistance exceeds , the transfer pump halts within .
# 7. Do's and Don'ts for Static Safety
| Operation | DO | DON'T |
|---|---|---|
| Liquid Transfer | • Use dip tubes extending to within 50 mm of the vessel bottom. • Ground all piping flanges and bridge with copper jumper straps. • Maintain relaxation time of before sampling. | • Do not splash fill solvents from top nozzles. • Do not exceed 1.0 m/s flow velocity before submerging the nozzle. • Do not use ungrounded flexible hoses. |
| Solid Dosing | • Verify oxygen concentration is less than 3% via nitrogen purge. • Use grounded Type C FIBC bags or closed PTS systems. | • Do not pour dry powders into flammable headspace manually. • Do not use ungrounded non-conductive plastic bags. |
| Filtration & Drying | • Ground the filter plate, ANFD shell, and centrifuge basket. • Use conductive filter cloths with interwoven stainless steel fibers. | • Do not open the filter dryer hatch before verifying solvent vapors are gone. • Do not use ungrounded filter bags or non-conductive drive belts. |
| Operator Safety | • Wear static-dissipative safety shoes (). • Verify ground loop resistance is less than 10 Ohms via daily ESD turnstile. | • Do not use plastic scoops, synthetic brushes, or insulated tools. • Do not wear synthetic garments (nylon/polyester) in classified zones. |
# 8. Reference Standards Used
- NFPA 77: Recommended Practice on Static Electricity.
- API RP 2003: Protection Against Ignitions Arising out of Static, Lightning, and Stray Currents.
- CENELEC CLC/TR 60079-32-1: Explosive atmospheres - Electrostatic hazards, guidance.
# Applicable Engineering Standards & Codes Used
The engineering methodologies, design correlations, and safety criteria detailed in this article adhere to the following international standards and industry codes:
- US FDA 21 CFR Part 211: Current Good Manufacturing Practice for Finished Pharmaceuticals
- EU GMP Annex 1: Manufacture of Sterile Medicinal Products
- ISPE Baseline Pharmaceutical Engineering Guide (Vol 1-7: Bulk Active Pharmaceutical Ingredients, Water & Steam Systems): ISPE Baseline Pharmaceutical Engineering Guide (Vol 1-7: Bulk Active Pharmaceutical Ingredients, Water & Steam Systems)
- WHO Technical Report Series No. 961: Supplementary Guidelines on Good Manufacturing Practices for Heating, Ventilation and Air Conditioning