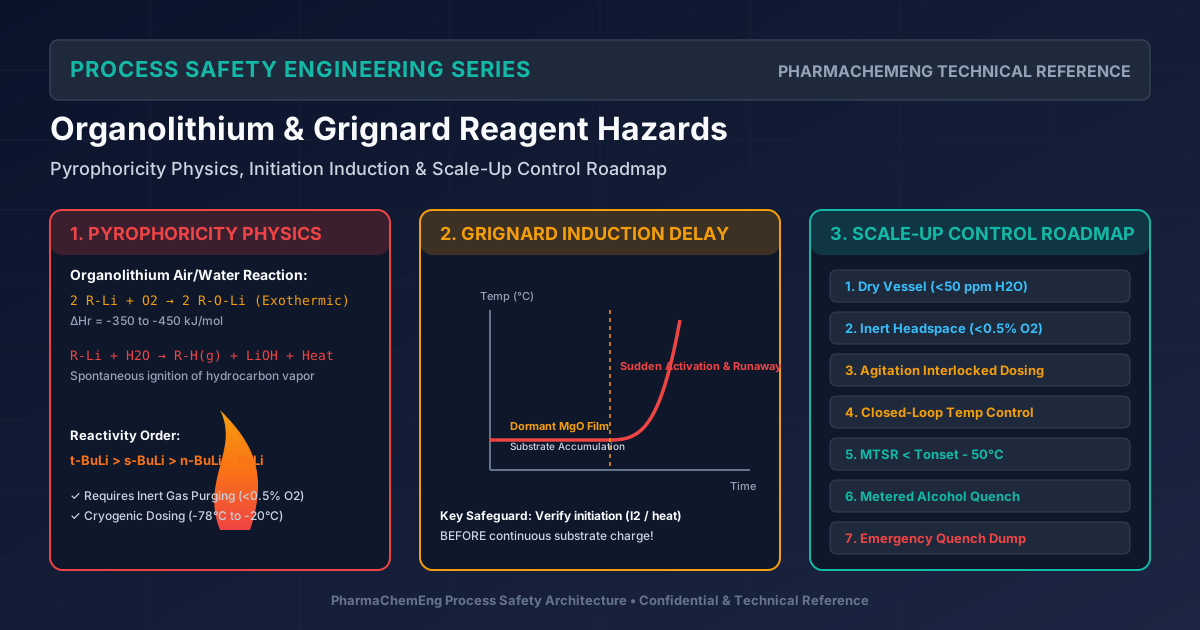
# Safe Scale-Up of Pyrophoric Organolithium & Grignard Reagents in API Manufacturing
# Executive Summary & Chemical Process Safety Context
Organometallic reagents—specifically organolithium compounds (-butyllithium, -butyllithium, -butyllithium, methyllithium, phenyllithium) and Grignard reagents (organomagnesium halides, )—are indispensable synthetic tools in commercial Active Pharmaceutical Ingredient (API) manufacturing. They drive essential carbon–carbon bond formations, stereoselective alkylations, low-temperature Directed ortho-Metalations (DoM), and halogen-metal exchange reactions that cannot be achieved via classical nucleophilic substitution pathways.
However, these reagents exhibit some of the most unforgiving reactive chemistry hazards in the chemical industry: extreme pyrophoricity upon atmospheric contact, violent water reactivity with simultaneous flammable alkane gas evolution, unpredictable induction periods in Grignard initiation leading to runaway autocatalytic thermal explosions, and severe cryogenic heat transfer constraints during industrial semi-batch additions.
+--------------------------------------------------------------------------------------------------+
|                     ORGANOMETALLIC PROCESS HAZARDS IN API SCALE-UP                                |
+--------------------------------------------------------------------------------------------------+
|  1. ATMOSPHERIC PYROPHORICITY  ==> Instantaneous flash ignition upon ambient air contact (<0.5 s)|
|  2. INDUCTION TRAP (GRIGNARDS) ==> MgO oxide passivation causes reagent accumulation (Y_acc -> 1)|
|                                ==> Autocatalytic initiation triggers massive thermal explosion   |
|  3. CRYOGENIC HEAT TRANSFER    ==> Reactor U-values drop 60-70% at -70°C to -40°C               |
|                                ==> Dosing rate must be strictly governed by U * A * ΔT_jacket    |
|  4. OFF-GAS FLAMMABILITY       ==> Stoichiometric alkane release (butane, methane, ethane)       |
|                                ==> Continuous N2 dilution sweep required to maintain < 25% LEL   |
|  5. WORKUP & QUENCH SHOCK      ==> Direct water addition causes vapor explosions & LiOH crusting |
|                                ==> Requires strict 4-Tier Quenching Hierarchy                    |
+--------------------------------------------------------------------------------------------------+
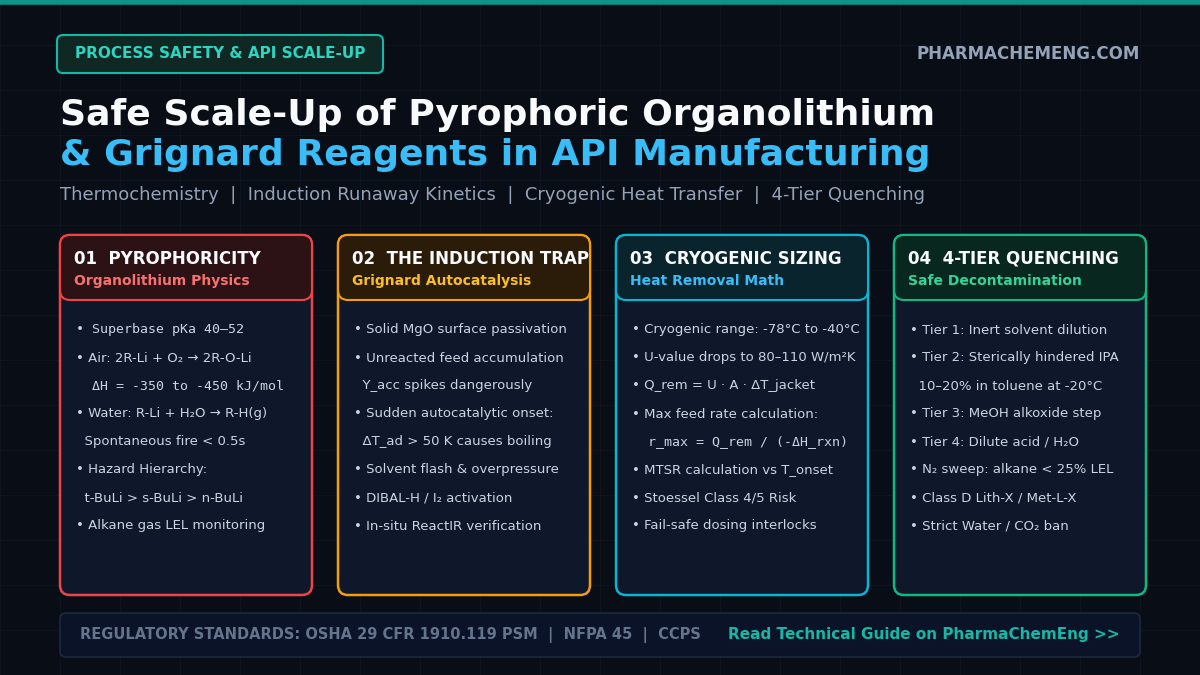
This engineering guide provides process development chemists, chemical process engineers, and EHS safety directors with an exhaustive, quantitative framework for characterizing, designing, scaling up, and safely operating organometallic reaction steps in pilot plants and commercial API manufacturing facilities.
# 1. Organolithium Reactivity & Pyrophoricity Physics
# 1.1 Superbasicity & Polar Covalent Bond Physics
Organolithium reagents are among the strongest known organic bases and nucleophiles, exhibiting conjugate acid values spanning 42 to 52. The polar covalent bond between carbon (Pauling electronegativity 2.55) and lithium (Pauling electronegativity 0.98) possesses approximately ionic character:
This high localized electron density on the carbanionic center gives rise to instantaneous proton abstraction from any available protic source (, alcohols, amines, terminal alkynes, enolizable ketones) and spontaneous addition across multiple bonds.
# 1.2 Aggregation States & Solvent Coordination Dynamics
In the condensed phase, organolithium reagents do not exist as simple isolated monomers. Due to electron deficiency on the lithium center (having only four valence electrons in classical covalent configurations), the molecules associate into stable supramolecular oligomers:
      [ Hydrocarbon Solvents: Hexane / Heptane ]
                 (n-BuLi)6 Hexamer  <--->  (t-BuLi)4 Tetramer
                               |
                        + Lewis Base (THF, TMEDA, DME)
                               v
      [ Polar Coordinating Solvents ]
                 (n-BuLi)2 Dimer    <--->  (n-BuLi · 2TMEDA) Monomer
                 (Reactivity accelerates by 10^2 to 10^4!)
Non-Polar Hydrocarbon Solvents (Hexane, Heptane, Cyclohexane):
- -BuLi forms hexameric prisms, .
- -BuLi and -BuLi, due to steric hindrance, form tetrahedral tetramers, and .
- These aggregates have lower nucleophilic addition rates at ambient temperatures, but retain extreme chemical potential when exposed to atmospheric oxidizers.
Polar Coordinating Solvents (THF, 2-MeTHF, Diethyl Ether, TMEDA):
- Lewis basic lone pairs donate electron density into vacant lithium orbitals, deaggregating bulky hexamers and tetramers down to reactive dimers and solvated monomers:
- Scale-Up Warning: Addition of co-solvents like Tetramethylethylenediamine (TMEDA) or switching from heptane to THF increases the deprotonation rate constant () by up to four orders of magnitude, transforming a moderately controlled dosing regime into an instantaneous, heat-transfer-limited reaction.
# 1.3 Thermochemistry of Air Exposure & Flash Pyrophoricity
When organolithium solutions are released into open air, two competing, fiercely exothermic reactions occur concurrently:
- Oxidative Degradation:
- Hydrolysis with Atmospheric Moisture:
The tremendous heat liberated by these concurrent reactions ( combined) immediately vaporizes the volatile hydrocarbon carrier solvent (pentane, hexane, heptane) and produces hot alkane gas. Because the adiabatic local temperature exceeds the autoignition temperature (AIT) of the hydrocarbon solvent (e.g., -pentane ; -hexane ), the vapor mixture ignites spontaneously within milliseconds.
# 1.4 Comprehensive Organometallic Reagent Hazard Matrix
| Reagent | Commercial Form | Conjugate Acid | Hydrolysis Enthalpy () | Pyrophoric Ignition Delay | Evolved Off-Gas | Gas LEL / UEL (vol%) |
|---|---|---|---|---|---|---|
| -Butyllithium (-BuLi) | in Hexanes | on porous surfaces; burns vigorously | -Butane () | |||
| -Butyllithium (-BuLi) | in Cyclohexane | ; rapid open-air ignition | -Butane / Isobutane | |||
| -Butyllithium (-BuLi) | in Pentane | (Spontaneous fireball on tip) | Isobutane () | |||
| Methyllithium (MeLi) | in Diethyl Ether | Highly pyrophoric; ignites ether carrier | Methane () | |||
| Phenyllithium (PhLi) | in Dibutyl Ether | Moisture sensitive; ignites wipes & cotton | Benzene () | |||
| Methylmagnesium Chloride | in THF | Non-pyrophoric; violent foaming & steam | Methane () | |||
| Ethylmagnesium Bromide | in Diethyl Ether | Slow aerosol ignition; flashes if misted | Ethane () | |||
| Phenylmagnesium Bromide | in 2-MeTHF | Hydrolyzes violently with boiling solvent | Benzene () | |||
| Lithium Diisopropylamide (LDA) | in THF/Heptane | Strong base; flammable vapor generation | Diisopropylamine |
# 2. Grignard Initiation Hazards & The Induction Runaway Trap
# 2.1 The Solid-Liquid Single Electron Transfer (SET) Mechanism
The classical preparation of a Grignard reagent involves reacting magnesium turnings with an organic halide in an anhydrous ethereal solvent:
The accepted mechanistic pathway proceeds through a multistep radical pair on the metal surface:
Mg(solid) + R-X ---> [ Mg•+ (R-X)•- ]_surface ---> [ Mg•+ R• X- ] ---> R-MgX (solution)
Because magnesium is a solid reactant, the reaction takes place strictly at the phase boundary.
+--------------------------------------------------------------------------------------------------+
|                            THE DEADLY GRIGNARD INDUCTION LOOP                                    |
+--------------------------------------------------------------------------------------------------+
|                                                                                                  |
|   1. MgO/Mg(OH)2 Passivated Turnings Charged + Solvent                                           |
|                           |                                                                      |
|                           v                                                                      |
|   2. 10% Halide Added ---> NO REACTION OBSERVED (Heat Generation = 0 kW)                         |
|                           |                                                                      |
|   [FATAL MISTAKE]         v                                                                      |
|   3. Operator continues feeding R-X  ===> ACCUMULATION FRACTION Y_acc SPIKES TO 80 - 100%        |
|                           |                                                                      |
|                           v                                                                      |
|   4. Localized Pitting Breaks Oxide Film (Tipping Point Reached)                                 |
|                           |                                                                      |
|                           v                                                                      |
|   5. AUTOCATALYTIC INITIATION CASCADE: Massive Accumulated Mass Reacts in Seconds                |
|      ΔT_ad > 80 - 150 K  ===> Instantaneous Solvent Boiling & Extreme Vapor Overpressure         |
|      Result: Rupture Disk Blows, Vapor Cloud Explosion (VCE), or Reactor Rupture                 |
+--------------------------------------------------------------------------------------------------+
# 2.2 Mathematical Modeling of Induction Accumulation ()
The mass balance for the organic halide reactant () in a semi-batch Grignard reactor is:
Where:
- = Molar dosing rate of organic halide ()
- = Rate of Grignard formation ()
- = Active, unpassivated magnesium surface area ()
The unreacted accumulation fraction, , is defined as:
During the induction phase, the magnesium surface is passivated by a film of and . Therefore, , which forces:
If the entire stoichiometric charge of is added during an unrecognized induction delay, the adiabatic temperature rise () upon sudden initiation is:
For an industrial batch of 4-chlorotoluene Grignard in THF (, , , ):
If initiation occurs at an initial batch temperature of :
Because THF boils at at atmospheric pressure, heating the batch to generates a saturated THF vapor pressure of:
This exceeds the standard design pressure of glass-lined steel reactors () and catastrophic vessel rupture or blowout of rupture disks is guaranteed.
# 2.3 Activation Protocols & Real-Time PAT Verification
To eliminate the induction delay and prevent dangerous reactant accumulation, chemical plants must enforce strict activation and verification rules:
+--------------------------------------------------------------------------------------------------+
|                    MAGNESIUM ACTIVATION METHODS IN COMMERCIAL API PLANTS                         |
+--------------------------------------------------------------------------------------------------+
|  METHOD 1: DIBAL-H Chemical Depassivation (Industry Standard)                                    |
|  - Charge 1.0 - 2.0 mol% Diisobutylaluminum hydride (DIBAL-H in toluene) to Mg/solvent slurry    |
|  - DIBAL-H acts as a powerful hydride donor, stripping MgO/Mg(OH)2 films and creating hydride-   |
|    activated magnesium clusters in-situ within 5-10 minutes at 30-40°C.                          |
|                                                                                                  |
|  METHOD 2: 1,2-Dibromoethane (Sacrificial Halide)                                                |
|  - Charge 1 - 3 mol% 1,2-dibromoethane: Br-CH2-CH2-Br + Mg -> CH2=CH2(g) + MgBr2                |
|  - Generates harmless ethylene gas and etches the metal surface clean. Gas evolution provides    |
|    visual/pressure confirmation of active initiation.                                            |
|                                                                                                  |
|  METHOD 3: Iodine Crystal Etching                                                                |
|  - Charge 0.05 mol% crystalline I2: forms soluble MgI2, exposing pristine shiny metal.           |
|  - Discharge of reddish brown iodine color confirms surface activation.                          |
+--------------------------------------------------------------------------------------------------+
# The "5% Golden Rule" of Grignard Feeding:
- Charge solvent, magnesium turnings, and the activating agent (e.g., DIBAL-H).
- Charge exactly of the total organic halide quantity.
- STOP THE FEED PUMP.
- Monitor internal batch temperature () and jacket heat flux.
- Criteria for Confirmed Initiation:
- Measurable exotherm: without changing jacket temperature.
- Or in-situ ReactIR: Disappearance of halide stretch () and emergence of organomagnesium signature.
- Hard Interlock: If initiation is not verified within 15 minutes, dosing is prohibited, agitator is maintained, and root-cause troubleshooting begins. Never add more halide to an uninitiated batch!
# 3. Reaction Calorimetry (RC1) & Cryogenic Heat Transfer Mathematics
# 3.1 Semi-Batch Energy Balance in Jacketed Reactors
Semi-batch operation allows the rate of heat generation () to be controlled by metering the feed rate ():
Under steady, non-accumulating semi-batch dosing (), the heat generation rate is directly proportional to feed speed:
The heat removal rate from a jacketed API reactor is:
Where:
- = Overall heat transfer coefficient ()
- = Wetted heat transfer area ()
- = Batch operating temperature ()
- = Cooling jacket utility temperature ()
               FEED TANK (n-BuLi in Hexanes)
                          |
                    [Mass Flow Meter]
                          |
                   [FCV Interlocked]
                          |
                          v
         +----------------------------------+
         |   REACTION BATCH (THF, -70°C)     | <--- q_gen = (-ΔHr) * n_feed
         |                                  |
         |        [Cryogenic Jacket]        | ---> q_rem = U * A * (Tr - Tj)
         +----------------------------------+
# 3.2 The Cryogenic Heat Transfer Penalty
In organolithium chemistry (such as ortho-lithiation or asymmetric aldol additions), batch temperatures must often be maintained between and to suppress unwanted side reactions, elimination, or reagent decomposition.
Process chemists frequently assume that laboratory cooling capacity scales directly to pilot and commercial vessels. This is one of the most dangerous scale-up fallacies in pharma manufacturing.
+--------------------------------------------------------------------------------------------------+
|                   OVERALL HEAT TRANSFER COEFFICIENT (U) VS TEMPERATURE                           |
+--------------------------------------------------------------------------------------------------+
|  Operating Regime              Jacket Utility           U-Value (GLR)       U-Value (Hastelloy)  |
|  -----------------             --------------           -------------       -------------------  |
|  Steam Heating (+100°C)        Saturated Steam          350 - 450 W/m²K     500 - 650 W/m²K      |
|  Cooling Water (+25°C)         Tower Water              250 - 320 W/m²K     350 - 480 W/m²K      |
|  Brine Chilling (-15°C)        Propylene Glycol         140 - 180 W/m²K     200 - 280 W/m²K      |
|  CRYOGENIC (-70°C to -85°C)    Syltherm XLT / Dynalene  70 - 110 W/m²K      90 - 140 W/m²K       |
+--------------------------------------------------------------------------------------------------+
# Why -values collapse at cryogenic temperatures:
- Fluid Viscosity Surge: The kinematic viscosity () of thermal heat transfer fluids (e.g., Syltherm XLT, Therminol, or silicone oils) increases by as temperature drops from to .
- Laminarization of the Jacket Boundary Layer: Higher viscosity drastically lowers the jacket Reynolds number (), driving flow from turbulent into transitional or laminar regimes, slashing the jacket film coefficient () by up to .
- Process Side Viscosity: Organic solvents like THF or toluene thicken, increasing the batch boundary film resistance ().
# 3.3 Safe Permissible Dosing Rate Derivation
To prevent loss of temperature control, the instantaneous heat generation must never exceed the available cooling duty:
Solving for the maximum allowable volumetric feed rate ( in or ):
Where is reagent concentration () and is the molar enthalpy of reaction ().
# 3.4 Stoessel Criticality Matrix Assessment
The Swiss process safety framework developed by Francis Stoessel classifies chemical processes based on four characteristic temperatures:
- = Normal process operating temperature
- = Boiling temperature of the metered reactant
- = Maximum Temperature of the Synthesis Reaction upon complete loss of cooling:
- = Onset temperature of catastrophic secondary thermal decomposition (measured by DSC or ARC)
- = Atmospheric or setpoint boiling point of the reaction mixture
   TEMPERATURE SCALE:

   [ T_p: -70°C ]  ----->  [ MTSR: -20°C ]  ----->  [ T_b: +66°C (THF) ]  ----->  [ T_D: +95°C (Decomp) ]
      |                         |                        |                              |
      Normal Process       Max Temp after           Solvent Reflux/Boil            Runaway Explosion
      Cryogenic Run        Cooling Failure          Cooling Envelope               Tipping Point
| Stoessel Class | Criteria Condition | Safety Implications & Engineering Controls Required |
|---|---|---|
| Class 1 | and | Inherently safe by design. Even with 100% accumulation, decomposition cannot trigger. |
| Class 2 | Boiling solvent provides evaporative evaporative tempering before decomposition can occur. | |
| Class 3 | Overpressurization risk due to boiling solvent vapor, but secondary explosion is avoided. | |
| Class 4 | High risk! If cooling is lost, batch exceeds decomposition onset before solvent boiling can temper. | |
| Class 5 | EXTREME CRITICALITY. Thermal runaway to explosion is inevitable upon loss of cooling. |
Organolithium Scale-Up Reality: Because organolithium decompositions (e.g., -BuLi deprotonating THF at to produce ethylene and acetaldehyde enolate in an explosive chain) have low onset temperatures ( to ), semi-batch additions frequently belong to Stoessel Criticality Class 4 or 5. Strict dosing interlocks and emergency quench loops are mandatory!
# 4. Rigorous Worked Engineering Case Study: 3,000 L Cryogenic Alkylation in Hastelloy C-22
# 4.1 Plant Scenario & Chemical Transformation
An API intermediate undergoes an ortho-directed lithiation followed by an electrophilic aldehyde addition. The reaction uses -butyllithium ( in hexanes) in anhydrous THF under dry argon atmosphere.
                  Base Substrate in THF (1,800 L) at -70°C
                                   +
                    n-BuLi (2.5 M in Hexanes, 450 L)
                                   |
                                   v  (-70°C, ΔHr = -195 kJ/mol)
                   Lithio-Intermediate + n-Butane (dissolved)
+--------------------------------------------------------------------------------------------------+
|                               DESIGN SPECIFICATIONS & PROCESS DATA                               |
+--------------------------------------------------------------------------------------------------+
|  Reactor Type:                 3,000 L Hastelloy C-22 Cryogenic Reactor (DIN EN ISO 10628)       |
|  Vessel Internal Diameter (D): 1.50 m                                                            |
|  Reactor Straight Side (H):    1.80 m                                                            |
|  Initial Batch Volume (V_0):   1,800 L (THF + Substrate slurry)                                  |
|  Reagent Volume to Charge:     450 L of 2.5 M n-BuLi (1,125 moles n-BuLi)                        |
|  Final Batch Volume (V_f):     2,250 L                                                           |
|  Operating Temperature (T_p):  -70.0°C (203.15 K)                                                |
|  Max Allowable Batch Temp:     -60.0°C (213.15 K) (to prevent THF cleavage decomposition)        |
|  Thermal Fluid:                Syltherm XLT Heat Transfer Fluid                                  |
|  TCU Supply Temperature (T_j): -85.0°C (188.15 K)                                                |
|  Available ΔT_driving:         T_p - T_j = -70.0°C - (-85.0°C) = 15.0 K                          |
|  Enthalpy of Reaction (ΔH_r):  -195.0 kJ/mol n-BuLi                                              |
|  Batch Density (ρ_batch):      910 kg/m³                                                         |
|  Batch Specific Heat (C_p):    2.05 kJ/kg·K                                                      |
|  Heat Transfer Coeff (U):      95.0 W/m²·K (Cryogenic Syltherm XLT / Hastelloy C-22)             |
+--------------------------------------------------------------------------------------------------+
# 4.2 Step 1: Wetted Heat Transfer Area () Calculation
For a dished-end cylindrical vessel, the effective heat transfer area increases as reagent is fed:
- Initial Wetted Area () at :
- Bottom 2:1 semi-ellipsoidal head area:
- Bottom head volume:
- Straight side liquid height ():
- Cylindrical wetted area:
- Total initial area:
- Final Wetted Area () at :
- Added volume in cylinder:
- Added height:
- Added area:
- Final area:
To ensure conservative safety margins, all sizing must be based on the minimum wetted area:
# 4.3 Step 2: Maximum Cooling Heat Removal Capacity ()
Using the cryogenic overall heat transfer coefficient :
# 4.4 Step 3: Permissible -BuLi Dosing Rate Calculation
Equating maximum heat generation to cooling capacity under non-accumulating steady feed ():
Convert molar dosing rate to volumetric flow rate of -BuLi solution:
Total required charge volume = .
Minimum safe semi-batch addition duration ():
# 4.5 Step 4: MTSR and Thermal Runaway Consequence Modeling
What happens if the cooling chiller trips 50% through the addition, with an undetected accumulation of ( unreacted -BuLi in solution)?
- Total moles accumulated:
- Instantaneous Heat Released:
- Current Batch Mass at 50% Addition:
- Adiabatic Temperature Rise ():
- Maximum Temperature of the Synthesis Reaction ():
Result Analysis: Because (the decomposition onset temperature), a 20% accumulation failure can be safely absorbed by the thermal inertia of the batch without crossing into catastrophic decomposition!
Catastrophic Scenario: If an operator charged the full in batch mode without cooling:
At , -BuLi aggressively cleaves THF, liberating gaseous ethylene and triggering secondary exothermic decomposition (), causing a violent thermal explosion.
# 5. Closed-Loop Hardware, Piping Design & Relief Sizing
  ARGON INERTING SKID (P > 3.0 barg)
                |
                v
  +---------------------------+       MASS FLOW METER (Coriolis)
  | ORGANOLITHIUM ISO-CONTAINER| ====> [ FTI-101 ] ====> PNEUMATIC SHUTOFF [ XV-101 ]
  +---------------------------+                                 |
         | (Dip Tube)                                           v
         +===========================================> [ CRYOGENIC REACTOR R-101 ]
                                                                |
                                                 DUAL RELIEF SYSTEM [ PRV / DISK ]
                                                                |
                                                                v
                                                 [ EMERGENCY QUENCH CATCH TANK ]
# 5.1 Pressure Transfer vs Canned Motor Pumping
Direct mechanical pumping of concentrated organolithium reagents introduces severe seal failure hazards:
- Mechanical Seal Failure: Standard elastomeric O-rings (Viton, FKM, Nitrile) embrittle and crack at cryogenic temperatures or degrade in strong hydrocarbon bases. Seal leakage releases pyrophoric liquid directly to air.
- Recommended Transfer Mechanism: Inert Gas Pressure Displacement:
- Use high-purity dry Argon or Nitrogen (dew point , ).
- Pressurize the transport ISO-container or cylinder to .
- Liquid is displaced through a dedicated stainless steel dip tube without rotating seals.
- If pumping is unavoidable, use sealless canned motor pumps or magnetically coupled gear pumps constructed from Hastelloy C-276 with Kalrez 6375 perfluoroelastomers.
# 5.2 Piping Specifications (ASME B31.3 Category M Fluid Service)
Piping handling organometallics must conform to ASME B31.3 Category M High Hazard Service:
- Material of Construction: Seamless 316L Stainless Steel (ASTM A312 TP316L) or Hastelloy C-22 for low-temperature toughness (impact tested down to ).
- Joint Construction: 100% butt-welded piping wherever feasible. Flanged connections must be minimized and fitted with 316 SS Flange Spray Shields to prevent jet spray in case of gasket failure.
- Valving: Firesafe ball valves conforming to API 607 / ISO 10497 with live-loaded PTFE/Grafoil stem packing and extended bonnets for cryogenic service.
- Dry-Break Disconnect Couplings: Reagent feed lines must utilize dry-break couplings (e.g., TODO-MATIC or MannTek style) equipped with internal poppet valves that automatically seal both sides before disconnection, preventing droplet exposure.
# 5.3 Emergency Pressure Relief & Anti-Plugging Protection
Organometallic reactions present unique relief sizing challenges because unreacted reagents or basic byproducts (, , magnesium alkoxides) rapidly precipitate and foul standard relief valve seats:
+--------------------------------------------------------------------------------------------------+
|                    RELIEF NOZZLE PLUGGING PREVENTION ARCHITECTURE                                |
+--------------------------------------------------------------------------------------------------+
|                                                                                                  |
|   REACTOR VAPOR HEADSPACE                                                                        |
|             |                                                                                    |
|             v                                                                                    |
|   [ CONTINUOUS ARGON BLEED PURGE ] (5 Nm³/h to keep nozzle dry & vapor-free)                     |
|             |                                                                                    |
|             v                                                                                    |
|   [ REVERSE-ACTING TEFLON RUPTURE DISK ] (Burst setpoint: 4.5 barg at -20°C)                    |
|             |                                                                                    |
|             +---> [ PRESSURE TRANSMITTER PT-102 ] (Detects pinhole leaks/disk damage)            |
|             |                                                                                    |
|             v                                                                                    |
|   [ ASME SECTION VIII SAFETY RELIEF VALVE ] (Set at 5.0 barg, balanced bellows)                  |
|             |                                                                                    |
|             v                                                                                    |
|   [ SUBMERGED VENT LINE TO QUENCH CATCH TANK WITH NITROGEN SPRAY ]                               |
+--------------------------------------------------------------------------------------------------+
- Rupture Disk + Safety Valve Combination: The primary safety relief valve must be protected by an upstream reverse-buckling Hastelloy rupture disk to isolate the valve seat from sticky alkoxide vapors.
- Continuous Purge: A dry nitrogen/argon purge sweep must be maintained between the rupture disk and relief valve seat to ensure no moisture diffuses backward from the plant vent header.
# 6. 4-Tier Industrial Quench Protocol & Hydrocarbon Flammability Mitigation
Quenching unreacted organolithium or Grignard residues is statistically the phase where most plant flash fires and thermal runaways occur. Adding water directly to a batch containing active organometallics is catastrophic.
# 6.1 The 4-Tier Controlled Quench Sequence
+--------------------------------------------------------------------------------------------------+
|                        THE 4-TIER INDUSTRIAL QUENCH HIERARCHY                                    |
+--------------------------------------------------------------------------------------------------+
|                                                                                                  |
|  [ TIER 1: THERMAL MASS DILUTION ]                                                               |
|  - Dilute batch with 20 - 30 vol% cold, dry hydrocarbon solvent (Toluene or Heptane).            |
|  - Lowers reagent molarity below 0.5 M; increases total batch heat capacity.                     |
|                                                                                                  |
|  [ TIER 2: STERICAL-HINDERED PROTIC QUENCH (ISOPROPANOL) ]                                       |
|  - Feed 10 - 20 vol% anhydrous Isopropanol (IPA) diluted in Toluene at -10°C to 0°C.             |
|  - Bulky isopropoxide formation is slow, smooth, and easily managed by reactor jacket.          |
|  - Reaction: R-Li + (CH3)2CHOH ---> R-H(g) + (CH3)2CHOLi (ΔH = -175 kJ/mol)                      |
|                                                                                                  |
|  [ TIER 3: PRIMARY ALCOHOL COMPLETE CONVERSION (METHANOL) ]                                     |
|  - Once IPA exotherm decays, feed 5 - 10 vol% Methanol at 0°C to 10°C.                           |
|  - Rapidly consumes sterically shielded organometallic residues.                                 |
|                                                                                                  |
|  [ TIER 4: AQUEOUS PHASE INVERSION & SALT DISSOLUTION ]                                          |
|  - Meter chilled 5 wt% Citric Acid, NH4Cl, or Water at +5°C to +15°C under high agitation.      |
|  - Completely hydrolyzes lithium/magnesium alkoxides into water-soluble salts.                  |
|  - Acid prevents high local alkalinity from precipitating gelatinous LiOH/Mg(OH)2 emulsions.     |
+--------------------------------------------------------------------------------------------------+
# 6.2 Off-Gas Nitrogen Sweep Sizing Calculation
During the quench of of -BuLi, stoichiometric butane gas () is evolved:
Total butane gas generated at Standard Temperature and Pressure ():
If the Tier 2 IPA quench is dosed uniformly over (), the average butane gas release rate is:
The Lower Explosive Limit (LEL) of -butane in air is .
Per NFPA 69 (Standard on Explosion Prevention Systems), the continuous inert purge rate must maintain the combustible gas concentration at or below of the LEL ():
Solving for the required Nitrogen purge flow rate ():
# 7. Emergency Response, Firefighting & Class D Agent Chemistry
# 7.1 Why Standard Fire Extinguishers Fail Catastrophically
Deploying common fire extinguishing agents on organolithium or Grignard fires causes violent physical and chemical explosions:
+--------------------------------------------------------------------------------------------------+
|                 PROHIBITED FIRE EXTINGUISHING MEDIA FOR ORGANOMETALLICS                          |
+--------------------------------------------------------------------------------------------------+
|  WATER & WATER FOAM:                                                                             |
|  - Explosive reaction: generates flammable H2 and alkane gas plus extreme heat:                   |
|    R-Li + H2O ---> R-H(g) + LiOH (ΔH = -240 kJ/mol)                                              |
|    2 Li + 2 H2O ---> 2 LiOH + H2(g) (ΔH = -445 kJ/mol)                                           |
|  - The heat instantaneously detonates the H2 and alkane vapors, projecting burning metal shrapnel|
|                                                                                                  |
|  CARBON DIOXIDE (CO2):                                                                           |
|  - Organolithiums react violently with CO2 via nucleophilic addition to form lithium carboxylates:|
|    R-Li + CO2 ---> R-COOLi (ΔH = -220 kJ/mol)                                                    |
|  - High-pressure gas jet atomizes and disperses the pyrophoric liquid across the room.           |
|                                                                                                  |
|  HALOCARBONS (HALON / FM-200 / NOVEC 1230):                                                      |
|  - Halogen-metal exchange with organolithiums creates explosive poly-lithiated intermediates.    |
+--------------------------------------------------------------------------------------------------+
# 7.2 Class D Extinguishing Chemistry: Lith-X & Met-L-X
Only certified Class D metal fire extinguishing agents are permitted in facilities handling organometallics:
   [ CLASS D LITH-X EXTINGUISHING MECHANISM ]

   Layer of Fine Graphite Flakes
   ============================================  <--- Excludes atmospheric Oxygen (O2)
   Conductive Heat Sink Layer                    <--- Absorbs high-temperature thermal energy
   ============================================
   Molten / Pyrophoric Organolithium Pool        <--- Smothers without gas dispersion turbulence
- Lith-X Powder (Mandatory for Lithium & Organolithiums):
- Composition: Specially graded, dry graphite flake powder mixed with organic flow-control additives.
- Extinguishing Mechanism: When applied gently, the graphite particles coat the burning liquid. Graphite possesses high thermal conductivity, conducting heat away from the pool below its combustion temperature while creating a dense, oxygen-impermeable smothering crust.
- Met-L-X Powder (For Magnesium & Grignard Spills):
- Composition: Sodium chloride () particles coated with a thermoplastic polymer.
- Mechanism: The heat melts the polymer, fusing the crystals into an airtight glassy salt crust over the burning magnesium metal.
# 7.3 Personal Protective Equipment (PPE) Matrix
| Protection Zone | Required Specification | Failure Mechanism of Inadequate Equipment |
|---|---|---|
| Protective Coat / Outerwear | NFPA 2112 certified Flame-Resistant (FR) Nomex III A or CarbonX lab coat / coverall | Synthetic lab coats (polyester, nylon) melt onto skin, causing third-degree burns. |
| Hand Protection | Heavy-duty Silvershield / 4H inner liners covered by heavy aluminized leather or heavy Neoprene outer gloves | Thin disposable nitrile gloves dissolve instantly in hexanes and ignite when exposed to -BuLi. |
| Face & Eye Protection | Full-face polycarbonate chemical splash shield with chin protector over ANSI Z87.1 impact goggles | Safety glasses provide no protection against upward pressurized droplet jet fires. |
| Emergency Drenching | Emergency safety drench showers located within uninhibited travel distance | In case of clothes fire, extinguish with fire blanket / drop-and-roll; do NOT spray water on open reagent pool. |
# 8. Process Safety Consulting Audit Report (`DIERS-PSM-2026-OM-014`)
====================================================================================================
                        PHARMA CHEMICAL ENGINEERING PROCESS SAFETY AUDIT
                                    REPORT ID: DIERS-PSM-2026-OM-014
====================================================================================================
FACILITY:     Global API Manufacturing Facility, Block B Cryogenic Suite
UNIT OP:      3,000 L Hastelloy C-22 Reactor (R-101) Ortho-Lithiation Scale-Up
REAGENTS:     n-Butyllithium (2.5 M in Hexanes) / THF Carrier Solvent
DATE:         September 2026
STATUS:       FINAL HAZOP & COMMISSIONING AUDIT SIGN-OFF
====================================================================================================
# 8.1 10-Point Mandatory Commissioning Checklist
+----+---------------------------------------------------------------+----------+------------------+
| No | Safety Verification Parameter                                 | Status   | Engineer Sign-off|
+----+---------------------------------------------------------------+----------+------------------+
| 01 | Moisture verification in reactor & feed loop (Karl Fischer < 30 ppm)| PASS   | SK - Lead EHS    |
| 02 | Oxygen sensor interlock in reactor headspace (< 0.5 vol% O2)  | PASS     | RM - Automation  |
| 03 | Cryogenic Syltherm XLT TCU heat transfer verified (U = 95 W/m²K) | PASS   | SK - Lead EHS    |
| 04 | Mass flow Coriolis meter calibrated with automatic shutoff <0.5 s| PASS    | RM - Automation  |
| 05 | Agitator power interlock: feed trips upon power loss < 0.2 s   | PASS     | RM - Automation  |
| 06 | Emergency high-temperature trip interlock set at -60.0°C      | PASS     | RM - Automation  |
| 07 | Reverse-acting rupture disk (4.5 barg) intact with argon purge| PASS     | DL - Mechanical  |
| 08 | Emergency catch tank pre-charged with cold heptane quench mass| PASS     | DL - Mechanical  |
| 09 | Minimum 4 dedicated Class D Lith-X extinguishers staged within 5 m| PASS | SK - Lead EHS    |
| 10 | Secondary N2 dilution sweep commissioned to keep vent < 25% LEL| PASS     | SK - Lead EHS    |
+----+---------------------------------------------------------------+----------+------------------+
# 8.2 HAZOP Deviation & Consequence Analysis
GUIDE WORD:   MORE FLOW (Reagent overfeeding beyond heat removal capacity)
CAUSE:        Control valve FCV-101 failure in full open position.
CONSEQUENCE:  Batch temperature surges from -70°C to above -60°C. Secondary decomposition of THF
              cleavage begins. Pressure spike due to ethylene gas evolution.
SAFEGUARD:    Safety Instrumented System (SIS) independent high-temp transmitter TT-102 trips
              fail-close pneumatic emergency isolation valve XV-101 within 200 milliseconds.

GUIDE WORD:   NO AGITATION (Agitator drive motor mechanical shear pin trips)
CAUSE:        Bearing seizure or motor electrical fault during semi-batch dosing.
CONSEQUENCE:  Concentrated n-BuLi pools on top of static reaction surface. Unreacted reagent
              accumulates without heat transfer. When agitation restarts, massive localized
              reaction triggers immediate thermal explosion.
SAFEGUARD:    Undercurrent sensor CT-101 and shaft motion encoder interlocked to XV-101. Reagent
              feed immediately trips upon agitator speed drop below 60 RPM. Restart prohibited!
# 9. Summary Checklist & Operational Key Takeaways
- Verify Initiation Unconditionally: In Grignard chemistry, never dose beyond of total organic halide without verifying initiation by exotherm () or in-situ ReactIR. Unreacted accumulation () is a catastrophic bomb.
- Account for Cryogenic -Value Degradation: Overall heat transfer coefficients collapse to at to . Sizing feed rates based on ambient -values guarantees loss of temperature control.
- Inert Gas Pressure Transfer Only: Eliminate mechanical rotating pump seals. Use high-purity argon or nitrogen () to transfer pyrophoric liquids via dip tubes and 100% butt-welded lines.
- Enforce the 4-Tier Quenching Hierarchy: Always quench unreacted organometallics hierarchically: Inert Dilution Isopropanol Methanol Chilled Aqueous Acid. Direct water addition produces violent hydrocarbon vapor explosions.
- Class D Extinguishers Exclusively: Stage certified Lith-X (for lithium) and Met-L-X (for magnesium) extinguishers. Water, foam, , and halogenated agents are strictly prohibited.
- Continuous Nitrogen Sweep Below 25% LEL: Size nitrogen dilution sweeps to ensure evolved hydrocarbon gases (butane, methane, ethane) never exceed of the Lower Explosive Limit in downstream vent and scrubber headers.
# References & Regulatory Standards
- OSHA 29 CFR 1910.119: Process Safety Management of Highly Hazardous Chemicals.
- NFPA 45: Standard on Fire Protection for Laboratories Using Chemicals.
- NFPA 69: Standard on Explosion Prevention Systems.
- CCPS / AIChE: Guidelines for Process Safety in Batch Reaction Systems, Center for Chemical Process Safety.
- Stoessel, F.: Thermal Safety of Chemical Processes: Risk Assessment and Process Design, Wiley-VCH.
- ASME B31.3: Process Piping Guide for Category M High Hazard Fluids.
- API 520 / 521: Sizing, Selection, and Installation of Pressure-Relieving Devices in Refineries and Chemical Plants.