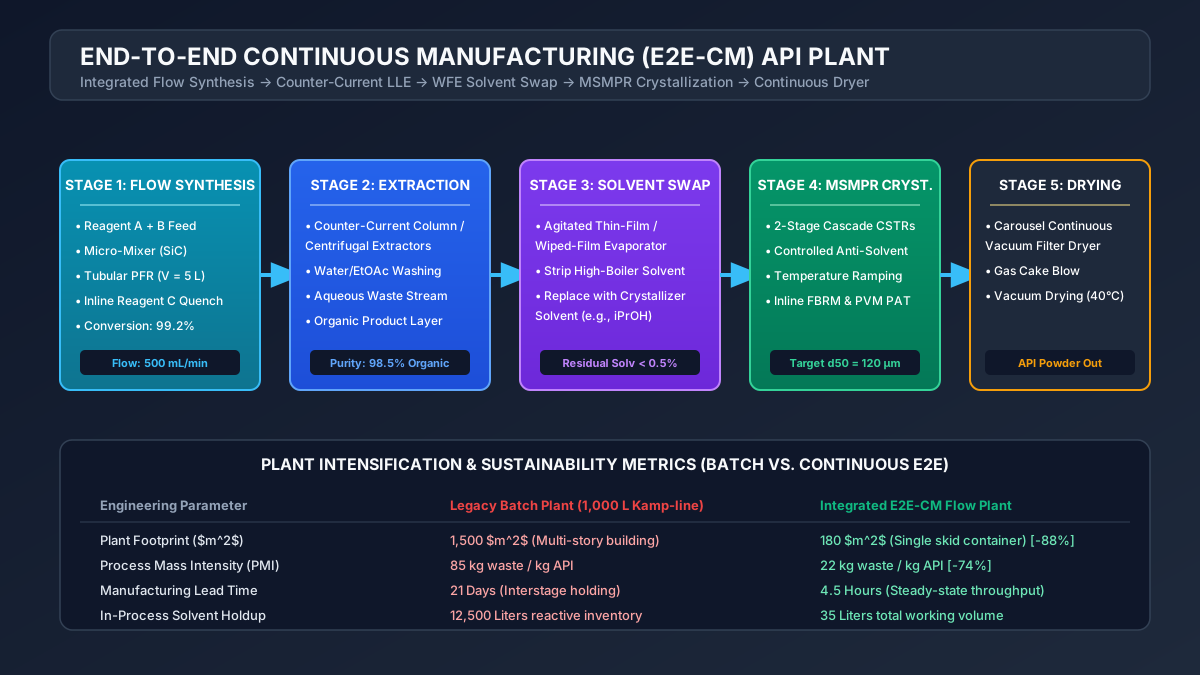
# End-to-End Continuous Manufacturing (E2E-CM) in API Plants: Integrated Flow Synthesis, Crystallization, Filtration & Drying
# An Advanced Chemical Engineering Blueprint on Residence Time Distributions (RTD), PFR/CSTR Cascades, Membrane Workup, MSMPR Dynamics, Continuous Deliquoring, and ICH Q13 Automated Material Diversion
# Executive Summary & Industrial Context
In traditional batch pharmaceutical manufacturing, the synthesis and isolation of an Active Pharmaceutical Ingredient (API) involves discrete, decoupled unit operations:
- Batch reactor synthesis (with extensive charging, heating, and cooling cycles),
- Quench and batch liquid-liquid phase separation,
- Batch crystallization inside jacketed stirred tanks,
- Solid-liquid separation in Agitated Nutsche Filter Dryers (ANFDs) or centrifuges,
- Batch vacuum tray or tumble drying, and
- Off-line intermediate sampling, QC hold periods, and manual material transfers.
This batch paradigm carries profound engineering and financial penalties: overall production lead times frequently span 30 to 90 days, equipment footprints require expansive multistory cleanrooms, work-in-progress (WIP) inventories tie up millions of dollars in capital, and transient scaling effects (such as non-uniform heat transfer, localized shear gradients, and extended hot spots) cause batch-to-batch variability and yield loss.
┌──────────────────────────────────────────────────────────────────────────────────────────────────┐
│                             BATCH VS. END-TO-END CONTINUOUS (E2E-CM)                             │
├────────────────────────────────┬────────────────────────────────┬────────────────────────────────┤
│ Engineering Metric             │ Conventional Batch Operation   │ Integrated E2E-CM Train        │
├────────────────────────────────┼────────────────────────────────┼────────────────────────────────┤
│ Manufacturing Lead Time        │ 30 – 90 Days                   │ 8 – 24 Hours                   │
│ Plant Cleanroom Footprint      │ 2,500 – 4,000 m²               │ 600 – 1,000 m² (-75%)          │
│ In-Process Chemical Holdup     │ 5,000 – 20,000 L               │ 50 – 250 L (-98%)              │
│ Specific Solvent Consumption   │ 12 – 25 kg solvent / kg API    │ 2.5 – 5.0 kg solvent / kg API  │
│ Heat Transfer Coefficient (U)  │ 150 – 400 W/(m²·K)             │ 1,500 – 5,000 W/(m²·K)         │
│ Thermal Runaway Risk           │ High (Large reactive mass)     │ Inherently Safe (Micro-holdup) │
│ Quality Verification           │ Retrospective (Offline QC)     │ Real-Time Release Testing (PAT)│
└────────────────────────────────┴────────────────────────────────┴────────────────────────────────┘
End-to-End Continuous Manufacturing (E2E-CM) integrates raw material chemical transformation, extraction/workup, crystallization, filtration, washing, and drying into a single, automated, continuous process line. The entire sequence operates under closed-loop steady state, transforming raw starting materials into dry, packaging-ready crystalline API within hours.
This publication provides chemical engineers, plant managers, and scale-up specialists with an end-to-end technical guide to designing, sizing, controlling, and validating an integrated E2E-CM facility in compliance with ICH Q13 regulatory standards.
# 1. Integrated Flowsheet & Process Architecture
An industrial E2E-CM API train connects five continuous unit operations via active pressure balancing, automated flow metering, and Process Analytical Technology (PAT) checkpoints:
                            END-TO-END CONTINUOUS API MANUFACTURING TRAIN
 ┌──────────────────────────────────────────────────────────────────────────────────────────────────┐
 │                                                                                                  │
 │  RAW REAGENTS               UNIT 1: REACTION            UNIT 2: WORKUP         UNIT 3: CRYSTAL.  │
 │  ┌──────────────┐          ┌────────────────┐          ┌────────────────┐     ┌────────────────┐ │
 │  │ Reagent A    │──Pump───►│ Tubular PFR /  │─────────►│ Membrane-Based │────►│ MSMPR Stage 1  │ │
 │  │ & Reagent B  │──Pump───►│ Microchannel   │ (Inline  │ Phase Separator│     │ (Nucleation)   │ │
 │  └──────────────┘          │ Reactor Skid   │  Quench) │ (Zaiput / CINC)│     └───────┬────────┘ │
 │                            └────────────────┘          └───────┬────────┘             │          │
 │                                                                │ Waste Layer          ▼          │
 │                                                                ▼ (Aqueous)    ┌────────────────┐ │
 │                                                               (To Effluent)   │ MSMPR Stage 2  │ │
 │                                                                               │ (Growth & Cool)│ │
 │                                                                               └───────┬────────┘ │
 │                                                                                       │ Slurry   │
 │                                                                                       ▼          │
 │  FINAL PACKAGING           UNIT 5: DRYING              DIVERSION UNIT         UNIT 4: FILTER     │
 │  ┌──────────────┐          ┌────────────────┐          ┌────────────────┐     ┌────────────────┐ │
 │  │ OEB 4 / 5    │◄─────────│ Continuous     │◄─────────│ High-Speed     │◄────│ Continuous     │ │
 │  │ Split-Valve  │ (Vacuum  │ Agitated Screw │ (PAT OOS │ 3-Way Diverter │     │ Rotary Drum /  │ │
 │  │ Drum Filling │ Discharge│ / Paddle Dryer │ Rejection│ Shuttle Valve  │     │ Carousel Filter│ │
 │  └──────────────┘          └────────────────┘  Stream) └───────┬────────┘     └────────────────┘ │
 │                                                                │                                 │
 │                                                                ▼ (OOS Slurry to Rework Tank)     │
 └──────────────────────────────────────────────────────────────────────────────────────────────────┘
# Key Engineering Interfaces:
- Reaction-to-Workup Interface: Pressure-regulated inline quenching stops kinetic side-reactions within milliseconds and prevents outgassing or solvent boiling.
- Workup-to-Crystallization Interface: A continuous phase separator removes spent aqueous salts while delivering an organic stream with zero droplet entrainment.
- Crystallization-to-Filtration Interface: A non-clogging, low-shear peristaltic or diaphragm slurry transfer system preserves crystal morphology and prevents attrition.
- Filtration-to-Drying Interface: Continuous deliquored cake scraping feeds directly into a vacuum drying screw without air exposure or environmental contamination.
# 2. Unit Operation 1: Continuous Flow Synthesis & Reaction Engineering
# 2.1 Reactor Hydraulics: Tubular PFR vs. CSTR Cascade
Choosing between a Plug Flow Reactor (PFR) and a cascade of Continuous Stirred Tank Reactors (CSTRs) depends on chemical reaction kinetics, exothermicity, and phase behavior:
- Tubular PFR / Microreactor: Ideal for fast, homogeneous, highly exothermic reactions (), where heat flux demands an exceptionally high surface-area-to-volume ratio ().
- CSTR Cascade: Required when solids or slurries precipitate during reaction, or when reaction kinetics are moderate () and require mechanical suspension.
                           PFR VS. CSTR CASCAL CONVERSION COMPARISON
                     (First-order reaction, k = 0.1 min⁻¹, Total Residence Time = 30 min)

   Conversion X (%)
    100 ┼───────────────────────────────────────────────────────────── PFR (95.0%)
        │                                                ╭─────────── 5 CSTRs (92.4%)
     90 ┼────────────────────────────────────╭───────────╯
        │                         ╭──────────╯ 3 CSTRs (87.5%)
     80 ┼──────────────╭──────────╯ 2 CSTRs (80.0%)
        │              │
     70 ┼──────────────╯ 1 CSTR (75.0%)
        │
      0 ┴──────────────┴──────────┴──────────┴──────────┴──────────┴────► Stage Count (N)
For an -stage equal-volume CSTR cascade running a first-order irreversible reaction (), the exit concentration from stage is governed by:
where is the residence time of each individual stage.
For an ideal Plug Flow Reactor:
# 2.2 Residence Time Distribution (RTD) & Bodenstein Number
In continuous manufacturing, maintaining narrow residence time distribution (RTD) is essential to ensure consistent conversion and impurity control. Non-ideal axial backmixing causes over-reaction and byproduct formation.
The extent of backmixing in tubular reactors is quantified by the Bodenstein Number () (or reactor Péclet number ):
Where:
- = Superficial fluid velocity ()
- = Reactor tube length ()
- = Axial dispersion coefficient ()
Bodenstein Number (Bo) Regimes:
  Bo < 10                Bo = 20 - 50             Bo > 100               Bo > 500
[Heavy Backmixing]     [Moderate Dispersion]    [Near Plug Flow]       [Ideal Plug Flow]
Equivalent to 1-3 CSTRs High byproduct profile  Standard Flow Tubular   Microreactor Skids
The dimensionless variance of the residence time distribution relates to via the closed-vessel dispersion relation:
To guarantee in tubular flow reactors operating at low laminar Reynolds numbers (), install static mixing inserts (such as Sulzer SMX or Kenics elements) or deploy pulsatile flow in coiled tubes (Dean vortices). Coiling generates secondary Dean vortices () that flatten the parabolic laminar velocity profile, cutting axial dispersion by up to .
# 2.3 Extreme Heat Removal in Exothermic Reactions
Consider an exothermic organometallic coupling or nitration reaction with reaction enthalpy and reagent concentration .
In a batch reactor, heat transfer area is limited to . If dosing is accelerated, heat generation outpaces cooling capacity, triggering a thermal runaway:
In a continuous microchannel reactor with hydraulic diameter :
With an overall heat transfer coefficient , the reactor can dissipate up to of reaction heat. The reaction can be run under intensified conditions (elevated temperatures and high concentrations) with adiabatic temperature rises suppressed to under .
# 3. Unit Operation 2: Continuous Workup, Extraction & Phase Separation
Liquid-liquid extraction and aqueous quenching are required to remove inorganic salts, catalysts, and unreacted reagents prior to crystallization.
# 3.1 Capillary Force Membrane Phase Separators
Traditional batch gravity settling tanks require hours of decantation and often form persistent rag layers. Continuous API platforms frequently use capillary-force membrane phase separators (such as Zaiput Flow Technologies).
                 CAPILLARY MEMBRANE PHASE SEPARATOR MECHANISM
           Aqueous + Organic Emulsion / Slurry Feed
                            │
                            ▼
 ┌──────────────────────────────────────────────────────────┐
 │               Top Channel (Retentate Layer)              │
 │  ══════════════════════════════════════════════════════  │
 │  ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲ ▲  │ ◄── Hydrophobic PTFE Membrane
 │  │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │ │  │    (Pore Size dp = 0.5 μm)
 │  Organic Permeate Layer (Wets and Passes Through)        │
 └──────────────────────────┬───────────────────────────────┘
                            ▼
                   Clean Organic API Stream (To Crystallizer)
The membrane separator uses a hydrophobic microporous fluoropolymer (PTFE) membrane. Because the organic phase wets the hydrophobic PTFE preferentially (contact angle ), while the aqueous phase is non-wetting (), capillary pressure acts as a physical barrier preventing water breakthrough:
Where:
- = Interfacial tension between aqueous and organic phases ()
- = Contact angle on PTFE
- = Nominal membrane pore radius ()
To maintain complete separation without solvent carryover, the operating transmembrane pressure () must satisfy:
An integrated differential pressure control valve dynamically modulates the backpressure on the retentate line to keep within this operating window, even during feed flow perturbations.
# 3.2 Multi-Stage Counter-Current Centrifugal Extractors
For reactions requiring multi-stage washing with small partition coefficients (), continuous centrifugal extractors (e.g., CINC or Rousselet Robatel) are arranged in series. Operating at centrifugal accelerations of , these units achieve equilibrium mass transfer in under 5 seconds residence time while separating emulsions that would take hours to resolve in a settling vessel.
# 4. Unit Operation 3: Continuous Crystallization (MSMPR & OBC)
Continuous crystallization controls the primary Critical Quality Attributes (CQAs) of the drug substance: polymorphic purity, Crystal Size Distribution (CSD), aspect ratio, and residual impurity entrapment.
# 4.1 Population Balance Equations in Mixed Suspension Mixed Product Removal (MSMPR)
An MSMPR crystallizer operates at steady state with continuous feed introduction and continuous product slurry withdrawal.
                  MSMPR POPULATION DENSITY LOGARITHMIC PLOT
   ln[n(L)]
     ▲
  n₀ ┼───\
     │    \
     │     \   Slope = - 1 / (G · τ)
     │      \
     │       \
     │        \
     │         \
     └──────────\───────────────────────────────────────► Crystal Size L (μm)
Assuming size-independent crystal growth rate (), negligible attrition, and steady-state operation, the 1D Population Balance Equation (PBE) reduces to:
Integrating with boundary condition :
Where:
- = Number population density at size ()
- = Linear crystal growth rate ()
- = Mean residence time ()
- = Secondary/primary nucleation rate ()
The characteristic mean crystal size () of a single MSMPR is:
# 4.2 Multi-Stage MSMPR Cascade for Particle Size Control
A single MSMPR produces a wide, exponential particle size distribution with a coefficient of variation . In downstream processing, wide distributions cause filter cloth blinding and non-uniform drying.
Cascading two or three MSMPR stages in series with controlled temperature or antisolvent profiles narrows the distribution () and boosts overall recovery yield:
                      TWO-STAGE MSMPR CRYSTALLIZATION SYSTEM
                           Cooling & Antisolvent Staging

    Feed Solution (50°C)
           │
           ▼
   ┌──────────────┐
   │ MSMPR Stage 1│  T₁ = 35°C, τ₁ = 45 min
   │ (Nucleation) │  High supersaturation (S₁ = 1.35)
   └──────┬───────┘  Controlled secondary nucleation zone
          │ Slurry Transfer Line (Ultrasonically Agitated)
          ▼
   ┌──────────────┐◄── Fresh Antisolvent Feed Dosing
   │ MSMPR Stage 2│  T₂ = 10°C, τ₂ = 75 min
   │ (Growth)     │  Low supersaturation (S₂ = 1.08)
   └──────┬───────┘  Desupersaturation & crystal growth
          │
          ▼ Slurry to Continuous Filter (L₄₃ = 185 μm, CV = 38%)
# 4.3 Inline Wet Milling for Controlled Seed Generation
A major operational hurdle in continuous crystallization is maintaining steady-state seed populations without periodic operator intervention.
By installing an inline rotor-stator wet mill on an external recycle loop around MSMPR Stage 1, a small fraction of large crystals is milled into micron-sized fragments () and returned to the vessel. This provides a continuous source of active seed surface area without introducing foreign seeds or triggering uncontrolled primary nucleation.
# 5. Unit Operation 4: Continuous Solid-Liquid Filtration & Washing
Continuous separation of crystalline API from mother liquor is accomplished using a Rotary Drum Vacuum Filter (RDVF), a Continuous Indexing Carousel Vacuum Filter, or a Continuous Belt Filter.
                   ROTARY DRUM VACUUM FILTER (RDVF) ZONES
                              (Continuous Cycle)

                       Wash Spray Manifolds
                             │  │  │
                             ▼  ▼  ▼
                   ┌─────────────────────────┐
                   │    WASHING ZONE (35%)   │
            ┌──────┴─────────────────────────┴──────┐
            │                                       │
            │                                       │  ◄── DRYING / DELIQUORING
   CAKE     │                                       │      ZONE (20%)
 DISCHARGE  │                                       │      (Gas Pull-Through)
   ZONE     │                                       │
   (15%)    │                                       │
            │                                       │
            └──────┬─────────────────────────┬──────┘
                   │    CAKE FORMATION       │
                   │      ZONE (30%)         │
                   └─────────────────────────┘
                               ▲
                               │ Slurry Trough (Continuous Feed)
# 5.1 Modified Ruth Filtration Equation for Continuous Cakes
In continuous rotary filtration, the cycle time is divided into three functional sectors: cake formation (), washing (), and deliquoring ().
The cake formation time is . Applying the Ruth filtration equation:
Where:
- = Active filtration area ()
- = Drum rotation speed ()
- = Applied vacuum differential ()
- = Mother liquor viscosity ()
- = Specific cake resistance (), with compressibility index
- = Mass of dry cake per unit filtrate volume ()
- = Clean filter cloth/support resistance ()
The dry solid production rate per unit filter area (, ) is:
# 5.2 Displacement Cake Washing Efficiency
Washing efficiency on continuous drum filters is modeled using the dispersion-displacement model:
Where:
- = Wash ratio (volume of wash solvent per unit cake void volume)
- = Péclet number of wash flow through the porous cake
- = Error function
During the final deliquoring sector, gas pull-through causes capillary menisci to contract within crystal interstices. For fine needle crystals (), non-uniform cake shrinkage produces structural fissures and cracks. Once cracked, vacuum short-circuits through fissures, ending deliquoring.
Engineering Fix: Install an automated mechanical compression belt or vibrating pneumatic smoothing roll across the deliquoring quadrant to close fissures and reduce cake moisture content from down to .
# 6. Unit Operation 5: Continuous Drying & API Discharge
Solid API discharged from continuous filtration typically retains residual solvent. Continuous drying brings residual moisture to within specification (, residual solvent ) without inducing thermal degradation, agglomeration, or solvate loss.
# 6.1 Equipment Selection: Vacuum Paddle vs. Vibrating Fluidized Bed vs. Oscillatory Screw
┌─────────────────────────────────┬─────────────────────────────────┬─────────────────────────────────┐
│ Continuous Dryer Type           │ Primary Heat Transfer Mode      │ Suitable API Characteristics    │
├─────────────────────────────────┼─────────────────────────────────┼─────────────────────────────────┤
│ Continuous Vacuum Paddle Dryer  │ Conduction via heated jacket &  │ Coarse, robust crystalline APIs;│
│ (Twin-Screw / Agitated Hollow)  │ hollow heated rotating blades   │ high thermal stability; solvent │
│                                 │ (U = 80 - 180 W/(m²·K))         │ recovery required under vacuum. │
├─────────────────────────────────┼─────────────────────────────────┼─────────────────────────────────┤
│ Vibrating Continuous Fluid Bed  │ Convective gas-solid transport  │ Free-flowing, non-sticky        │
│ Dryer (Vibrated Plug Flow)      │ (High gas velocity, N₂ closed)  │ spherical agglomerates; fragile │
│                                 │ (h = 150 - 350 W/(m²·K))        │ crystals; low boiling solvents. │
├─────────────────────────────────┼─────────────────────────────────┼─────────────────────────────────┤
│ Tubular Oscillatory Baffled     │ Conductive wall + convective N₂ │ Thermolabile, needle-like       │
│ Vacuum Dryer (TOBD)             │ gentle gas flow (pulsed bed)    │ crystals prone to attrition;    │
│                                 │ (U = 100 - 250 W/(m²·K))        │ low shear requirements.         │
└─────────────────────────────────┴─────────────────────────────────┴─────────────────────────────────┘
# 6.2 Heat & Mass Balance in a Continuous Paddle Dryer
For an API throughput of (dry basis) with an inlet solvent content and target outlet moisture :
The total evaporation rate is:
The thermal energy requirement accounts for sensible heating of solids and solvent, plus the latent heat of vaporization:
The required heat transfer surface area under vacuum is:
Where is the log-mean temperature difference between the heating utility jacket and the vacuum solvent evaporation temperature.
# 7. Process Analytical Technology (PAT) & Sensor Matrix
Under ICH Q13, continuous manufacturing processes rely on continuous monitoring rather than end-of-batch release testing. Real-time verification of intermediate streams ensures the process remains within its validated design space:
                        CONTINUOUS PAT SENSOR MATRIX (ICH Q13)
 ┌──────────────────────┬────────────────────────┬────────────────────────┬────────────────────────┐
 │ Unit Operation       │ In-Line Sensor Type    │ Target Critical Quality│ Feedback & Control     │
 │                      │                        │ Attribute (CQA)        │ Response Time          │
 ├──────────────────────┼────────────────────────┼────────────────────────┼────────────────────────┤
 │ Flow Synthesis Skid  │ Diamond ATR-FTIR       │ Reagent conversion,    │ Dosing pump micro-trim │
 │                      │ (Flow Cell)            │ byproducts, active API │ (< 2.0 s)              │
 ├──────────────────────┼────────────────────────┼────────────────────────┼────────────────────────┤
 │ Workup Separator     │ In-Line High-Frequency │ Phase boundary, aqueous│ Pressure regulator trim│
 │                      │ Conductivity & UV-Vis  │ carryover in organic   │ (< 500 ms)             │
 ├──────────────────────┼────────────────────────┼────────────────────────┼────────────────────────┤
 │ MSMPR Crystallizer   │ Focused Beam Refl.     │ Cord Length Dist. (CSD)│ Wet mill RPM & jacket  │
 │ (Stages 1 & 2)       │ (FBRM) & In Situ PVM   │ and polymorphic form   │ temperature (< 5.0 s)  │
 ├──────────────────────┼────────────────────────┼────────────────────────┼────────────────────────┤
 │ Continuous Filter    │ Diffuse Reflectance    │ Residual mother liquor │ Wash solvent valve trim│
 │                      │ Near-Infrared (NIR)    │ & wash displacement    │ (< 1.0 s)              │
 ├──────────────────────┼────────────────────────┼────────────────────────┼────────────────────────┤
 │ Continuous Dryer     │ Tunable Diode Laser    │ Loss on Drying (LOD) & │ Vacuum valve & jacket  │
 │                      │ (TDLAS) / Mass Spec    │ solvent off-gas content│ heating rate (< 1.5 s) │
 └──────────────────────┴────────────────────────┴────────────────────────┴────────────────────────┘
# 8. Dynamic Material Diversion & ICH Q13 Compliance
# 8.1 ICH Q13 Regulatory Principles: Defining a "Batch"
Under Section 3 of ICH Q13 (Continuous Manufacturing of Drug Substances and Drug Products), a continuous batch can be legally defined using any of three criteria:
- Time-Based Batch: All drug substance produced during a discrete, continuous operating window (e.g., 24-hour run time).
- Quantity-Based Batch: A defined mass or volume output (e.g., 500 kg of finished API).
- Raw Material Lot-Based: The total mass generated from a single defined lot of starting raw materials.
# 8.2 State of Control & Dynamic OOS Diversion Logic
A continuous process operates in a validated "State of Control" when all process variables remain within established design space boundaries, verified by in-line PAT.
When an upset occurs (e.g., pump flow drift, cooling failure, impurity spike), the control system must detect the disturbance and isolate the affected material before it enters downstream unit operations:
            DYNAMIC OUT-OF-SPECIFICATION (OOS) DIVERSION DECISION TREE
                                  (Automated DCS)

                      PAT Sensor Continuous Stream Reading
                                        │
                                        ▼
                      ┌──────────────────────────────────┐
                      │  Is Measured Parameter Inside   │
                      │  Validated Design Space (CQA)?   │
                      └─────────────────┬────────────────┘
                                        │
                       ┌────────────────┴────────────────┐
                       │ YES                             │ NO (Disturbance / OOS)
                       ▼                                 ▼
             [ Continue Forwarding ]           [ Activate 3-Way Diverter Valve ]
             (Downstream to Filter / Dryer)    (Transit time < 100 ms)
                                                         │
                                                         ▼
                                               [ Divert to Rework Tank ]
                                                         │
                                                         ▼
                                               [ Audit Trail Auto-Logged ]
                                               (ICH Q13 Incident Record)
# 8.3 Diverter Valve Latency Budget & Slug Segregation
To ensure that zero out-of-specification material contaminates the downstream drying unit, the total response latency () must be less than the fluid transport time () between the PAT probe and the diverter valve:
Where:
- = PAT instrument acquisition/integration time ()
- = Real-time spectral preprocessing and multivariate PLS model execution ()
- = Industrial DCS/PLC control scan cycle ()
- = Pneumatic high-speed 3-way shuttle valve firing time ()
The pipe length () between the PAT flow cell and the 3-way diverter valve must satisfy:
With a fluid velocity and a safety factor :
Installing at least of transfer line between the PAT probe and the 3-way valve guarantees that non-conforming slugs are diverted before reaching the downstream isolation unit.
# 9. Comprehensive Industrial Case Study: 15 kg/h Continuous API Line
To illustrate these engineering principles, consider a commercial continuous line synthesizing an active pharmaceutical intermediate:
- Target Output: dry API ().
- Reaction: Exothermic nucleophilic coupling in acetonitrile ().
- Crystallization: 2-Stage MSMPR cooling crystallization () with water antisolvent dosing.
- Separation: Rotary drum vacuum filtration with displacement washing.
- Drying: Continuous vacuum paddle dryer operating at and .
# 9.1 Equipment Sizing Summary
┌─────────────────────────┬─────────────────────────┬─────────────────────────┬─────────────────────────┐
│ Unit Operation          │ Sizing Basis / Model    │ Selected Equipment Spec │ Operating Setpoints     │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Unit 1: Flow Reactor    │ Tubular PFR with static │ Hastelloy C-276 Tube    │ Residence time: 4.5 min │
│                         │ mixing elements (Bo>120)│ L = 28 m, ID = 16 mm    │ T = 78°C, P = 6.5 bar g │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Unit 2: Phase Separator │ Capillary force PTFE    │ Zaiput Dual-Membrane    │ Flow rate: 68 L/h       │
│                         │ membrane separation     │ Active Area: 0.12 m²    │ ΔP_TMP = 120 mbar       │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Unit 3A: MSMPR Stage 1  │ Nucleation & seeding    │ 316L Jacketed MSMPR     │ V = 25 L, τ = 22 min    │
│                         │ with inline wet milling │ Agitator: Pitch Blade   │ T = 32°C, Mill: 3500 RPM│
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Unit 3B: MSMPR Stage 2  │ Growth & desupersat.    │ 316L Jacketed MSMPR     │ V = 50 L, τ = 44 min    │
│                         │ with antisolvent feed   │ Dual-Impeller Baffled   │ T = 10°C, S = 1.05      │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Unit 4: Rotary Filter   │ Cake filtration via     │ Continuous Rotary Drum  │ Active Area: 0.38 m²    │
│                         │ modified Ruth equation  │ Vacuum Filter (RDVF)    │ Speed: 1.2 RPM, Vac: 0.6│
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Unit 5: Continuous Dryer│ Conductive twin-screw   │ Agitated Vacuum Paddle  │ Heat Area: 1.25 m²      │
│                         │ paddle vacuum drying    │ Heated Jacket (Water)   │ T = 45°C, P = 30 mbar   │
└─────────────────────────┴─────────────────────────┴─────────────────────────┴─────────────────────────┘
# 9.2 Mass Balance Summary (Continuous Basis)
                       CONTINUOUS MASS BALANCE SUMMARY (15 kg/h DRY API)
 ┌──────────────────────┬──────────────────────┬──────────────────────┬──────────────────────┐
 │ Process Stream       │ Total Flow (kg/h)    │ Main Chemical Species│ Physical State       │
 ├──────────────────────┼──────────────────────┼──────────────────────┼──────────────────────┤
 │ Stream 1: Reagents   │ 48.5 kg/h            │ Reactants A + B + MeCN│ Homogeneous Liquid   │
 │ Stream 2: Quench     │ 15.0 kg/h            │ Aqueous NaHCO₃       │ Liquid Solution      │
 │ Stream 3: Aqueous Sep│ 18.2 kg/h            │ Spent salts + water  │ Aqueous Waste Layer  │
 │ Stream 4: Organic Sep│ 45.3 kg/h            │ Intermed. + MeCN     │ Clean Organic Layer  │
 │ Stream 5: Antisolvent│ 35.0 kg/h            │ Deionized Water      │ Liquid Feed          │
 │ Stream 6: Slurry     │ 80.3 kg/h            │ 18.7 wt% API Crystals│ 2-Phase Slurry       │
 │ Stream 7: Filtrate   │ 62.5 kg/h            │ MeCN + Water ML      │ Mother Liquor Waste  │
 │ Stream 8: Wet Cake   │ 17.8 kg/h            │ API + 15.7% Solvents │ De-liquored Wet Solid│
 │ Stream 9: Off-Gas    │ 2.8 kg/h             │ Evaporated Solvents  │ Vacuum Vapor Exhaust │
 │ Stream 10: Final API │ 15.0 kg/h            │ Pure Crystalline API │ Dry Solid (LOD<0.3%) │
 └──────────────────────┴──────────────────────┴──────────────────────┴──────────────────────┘
# 10. Operational Troubleshooting & Failure Modes Matrix
┌─────────────────────────┬─────────────────────────┬─────────────────────────┬─────────────────────────┐
│ Observed Anomaly        │ Root Cause Mechanism    │ Immediate Process Risk  │ Automated Engineering   │
│                         │                         │                         │ Intervention Strategy   │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Flow Reactor Back-      │ Premature precipitation │ Complete tube blockage, │ Ultrasonic clamp-on     │
│ pressure Creep          │ or insoluble byproduct  │ pressure safety valve   │ transducers; solvent    │
│ (> 1.5 bar increase)    │ encrustation on walls   │ lifting                 │ push purge sequence     │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Membrane Workup Water   │ Transmembrane pressure  │ Water carryover into    │ Automated ΔP valve      │
│ Breakthrough            │ exceeds capillary limit │ crystallizer causing    │ adjustment; switch to   │
│ (Conductivity Spike)    │ (ΔP_TMP > ΔP_cap)       │ uncontrolled seeding    │ standby dual separator  │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ MSMPR Vessel Encrust-   │ Excessive cooling-wall  │ Loss of heat transfer,  │ Dual crystallizers with │
│ ation / Scaling         │ supersaturation; no     │ drifting crystal size,  │ alternating hot-solvent │
│ (FBRM Count Decline)    │ scraping mechanism      │ sudden crystal shearing │ flush cycles (CIP)      │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Continuous Filter Cake  │ Fine needle morphology  │ Vacuum loss, bypass of  │ Engage mechanical       │
│ Cracking                │ shrinkage during gas    │ wash solvent, incomplete│ compression roller and  │
│ (Vacuum drops to zero)  │ pull-through drying     │ mother liquor removal   │ increase drum RPM       │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ Continuous Dryer Screw  │ API sticky zone entered │ Motor overload, thermal │ Modulate vacuum level   │
│ Torque Spike            │ due to excessive feed   │ decomposition of caked  │ and increase dry-solids │
│ (> 85% motor rating)    │ solvent moisture        │ API onto screw flights  │ recycle to reduce stick │
├─────────────────────────┼─────────────────────────┼─────────────────────────┼─────────────────────────┤
│ PAT Optical Window      │ Crystal accumulation on │ Blinded sensor, false   │ High-velocity automated │
│ Fouling                 │ probe sapphire face     │ OOS alarms, unnecessary │ solvent jet ring pulse  │
│ (ATR-FTIR / NIR Drift)  │                         │ diversion valve trips   │ cleaning across face    │
└─────────────────────────┴─────────────────────────┴─────────────────────────┴─────────────────────────┘
# 11. Engineering Rules of Thumb & Scale-Up Summary
- Volume Reduction & Safety: Expect an reduction in in-process reactive volume compared to equivalent batch equipment. A reaction that requires an batch vessel can typically be executed continuously in a total train volume.
- Residence Time Distribution: Keep in tubular sections to prevent over-reaction and impurity buildup. Use pulsatile flow or static mixing inserts when operating in laminar flow regimes.
- Crystallizer Sizing: Design the first MSMPR stage for nucleation and seed generation (), and subsequent stages for crystal growth (). Use an inline rotor-stator wet mill to generate seeds continuously without manual intervention.
- Filtration Cake Compressibility: If the cake compressibility index , do not increase vacuum differential; increasing vacuum compacts the cake and lowers throughput. Instead, decrease drum rotation speed to build a thinner cake () and employ mechanical compression rollers to eliminate fissures.
- ICH Q13 Diversion Design: Ensure transfer piping between PAT probes and 3-way diverter valves provides sufficient residence time to accommodate total sensor acquisition, computation, and valve actuation latency ().
- Redundancy by Design: Always design critical solid-handling units (wet mills, phase separators, and slurry pumps) with parallel dual-skids. This allows online cleaning or descaling without taking down the continuous train.
This guide is published by the PharmaChemEng Technical Editorial Board for chemical process development engineers, operational technology specialists, and regulatory compliance teams implementing continuous pharmaceutical manufacturing technologies.